Goji Pulp Buffer Tanks and Transfer
Stainless vessels and connected product pipework decouple uneven preparation from the more continuous treatment duty.
GOJI PROCESSING / Heat treatment
A tubular skid combines product heating, a defined holding duty and cooling interfaces with coordinated pumps and controls.
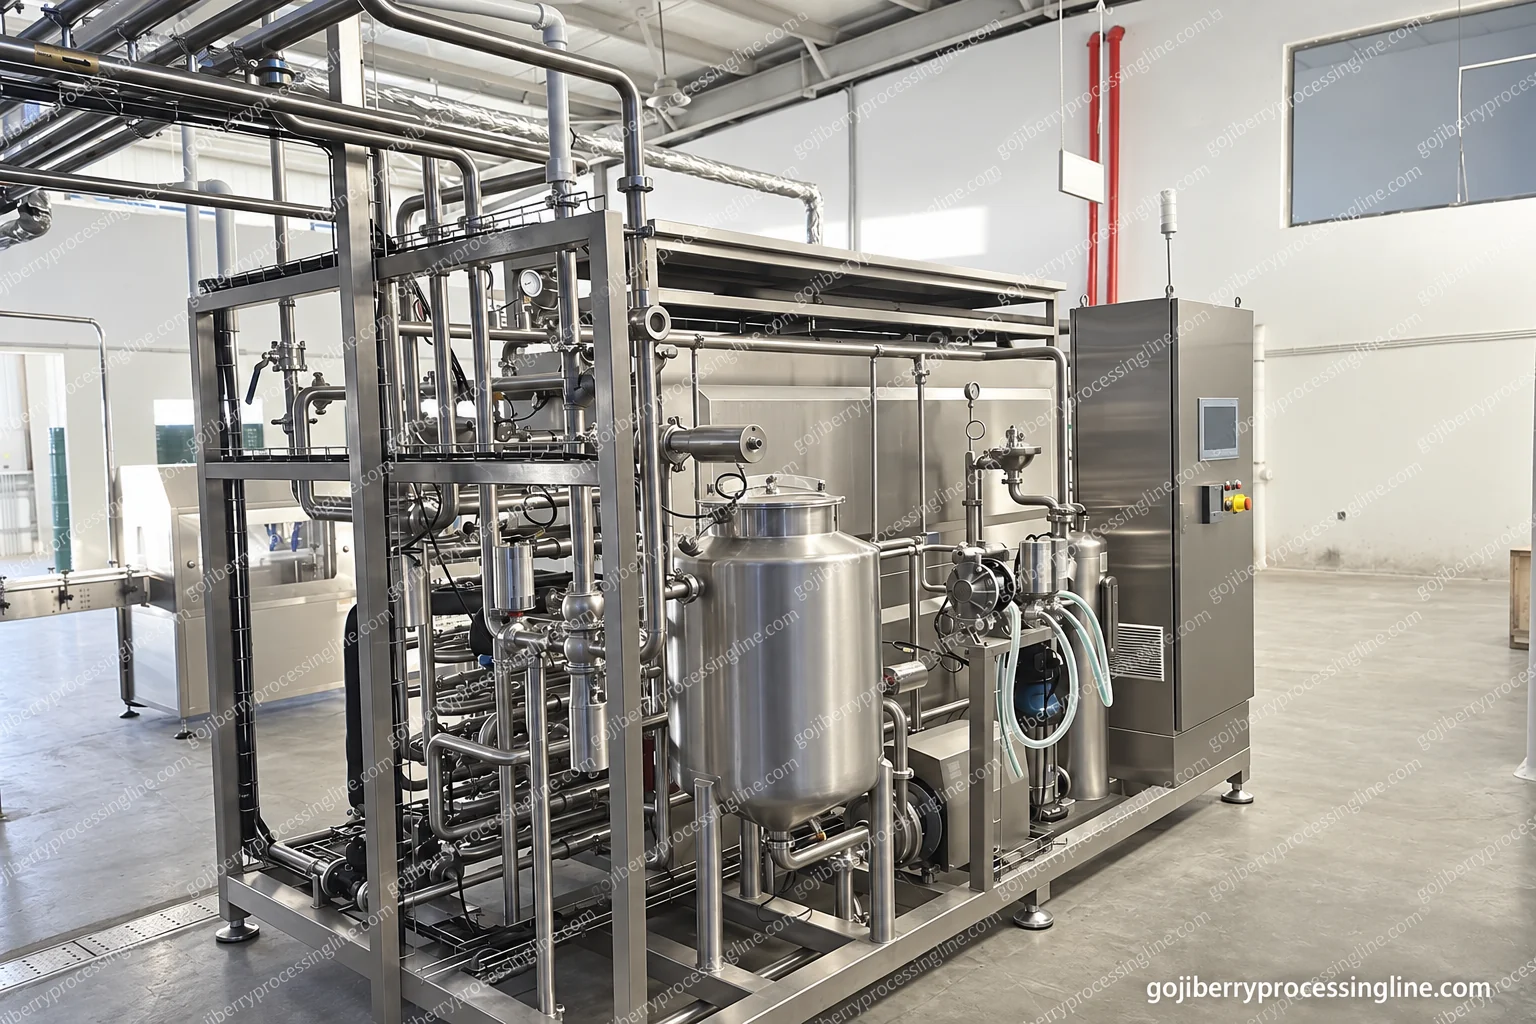
The tubular heat-transfer section brings the product toward its process temperature. The holding section provides the defined residence duty before cooling and discharge. Feed pump operation, temperature measurement and flow management determine whether the intended process conditions are actually met.
Start-up water, product below the release condition and cleaning liquid need appropriate routes. The controls must coordinate the heating medium, product flow and downstream availability. A hot skid alone does not establish that every product parcel meets a validated process.
Solids, fibres, particles, viscosity and fouling tendencies affect tube selection, pumping and cleaning. The process is selected against the target product, storage and packaging, including how the downstream filler maintains the required hygienic boundary.
| Family temperature reference | 72–150 °C |
|---|---|
| Family holding-time reference | 15–120 s |
| Product selection inputs | Viscosity, fibres/particles, flow and heat sensitivity |
| System interfaces | Product feed/outlet, heating medium, cooling and cleaning |
The visible assembly and equipment-family options guide selection; the selected model defines final dimensions, ratings and connections.
Verify temperature instruments, seals, accessible tube connections and the cleaning return. Make holding and diversion logic part of the selected system review. The listed ranges describe equipment-family options; they are not a goji sterilization schedule, guaranteed shelf life or ratings of the pictured skid.
No. It describes equipment-family temperature options. A product process must be established from the actual product, packaging, target organisms and validated conditions.
No. Shelf life depends on the complete product, process, filling, packaging and storage system. The site does not promise a shelf life from a temperature range.
The thermal outlet, product release, filler readiness, cleaning and sterile-utility boundary must be reviewed together. A generic skid image does not establish an aseptic arrangement.
Tell us the machine, product or starting material. The details can follow.